

Cellulose-Based Packaging Changes How Secondary Lines Run
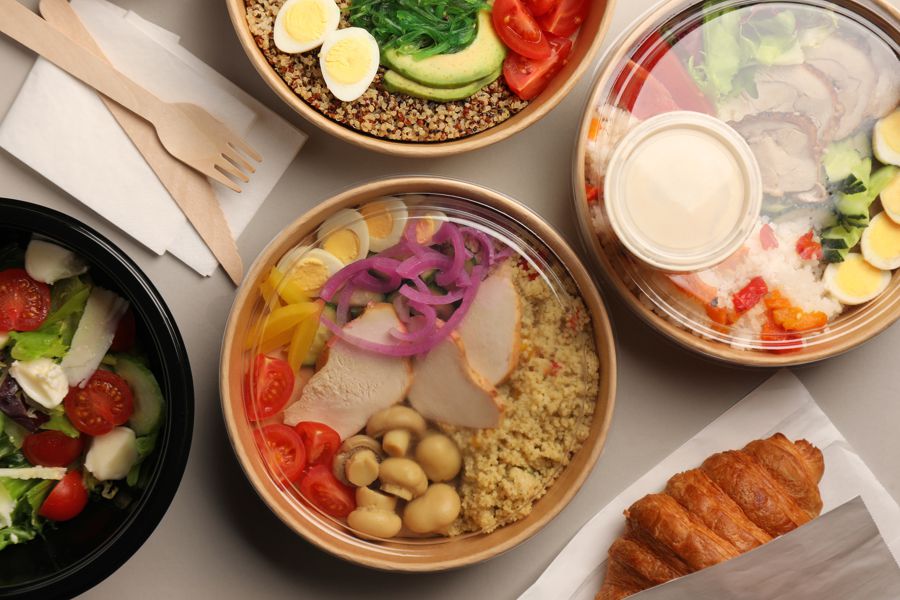
Cellulose-based packaging includes materials derived from wood pulp, cotton linters or agricultural fibres. formed into films, cartonboard, moulded trays or protective wraps. It's being adopted as a replacement for petroleum-based plastics in multipack overwraps, retail-ready cartons, and protective cushioning. The shift is driven by retailer mandates, extended producer responsibility legislation, and consumer preference for packaging that degrades or recycles within existing waste streams. For manufacturers running secondary packaging lines, the operational question is whether your existing machinery can handle them without performance loss.
Cellulose films behave differently than polyethylene or polypropylene under heat, tension, and compression. Cartonboard made from recycled or virgin cellulose varies in stiffness, surface friction, and moisture sensitivity compared to coated or laminated alternatives. If your cartoner, overwrapper, or tray former was specified around conventional substrates, switching to cellulose-based materials without addressing machine capability will result in slower line speeds, higher reject rates, or both. The cost of that performance gap often exceeds the material price difference, which means substrate decisions and machinery capability need to be evaluated together, not sequentially.
How Cellulose-Based Packaging Fits Within Secondary Operations
Cellulose-based packaging typically enters the line at secondary level. Primary packs (pouches, bottles, trays) are usually enclosed in cellulose film overwraps, loaded into cellulose-based cartons, or cushioned with moulded cellulose trays before moving to tertiary packaging. The machinery handling this work includes horizontal and vertical cartoners, shrink bundlers, tray formers, and multipack overwrappers. Each machine type interacts with cellulose substrates in ways that differ from conventional materials, and those differences affect speed, consistency, and changeover frequency.
Cellulose films, for example, have lower elongation at break than polyethylene, which means they're more prone to tearing under tension during film feed or heat sealing. Moulded cellulose trays have higher dimensional variation than plastic equivalents, which affects pick-and-place accuracy and nesting reliability. Recycled cartonboard with high cellulose content can be more prone to dust generation, which fouls sensors and affects vacuum cup performance on blank feeders. These are the operational realities that determine whether a substrate switch succeeds or stalls.
Secondary packaging machinery that handles cellulose materials reliably does so because it was designed or adapted to account for substrate variability. That includes adjustable film tension controls, servo-driven sealing heads that modulate heat and dwell time per material type, vacuum systems with filtration for dust-prone substrates, and forming rails with variable hold-down pressure to prevent panel collapse on lightweight board. If your machinery lacks these features, cellulose substrates will expose the gap between rated capability and actual performance.
What Breaks When Cellulose Substrates Aren't Matched to Machinery
The most immediate failure mode is film breakage during overwrapping. Cellulose-based films have narrower processing windows than conventional plastics—too much tension and they tear, too little and they don't conform to pack geometry. Overwrappers with fixed tension settings or mechanical clutch systems struggle to maintain the right balance across different cellulose film grades, which results in either torn film or loose packs that fail quality checks downstream.
Sealing consistency is the second common issue. Cellulose films and coatings require precise heat and pressure to form reliable seals. Too much heat degrades the material, too little results in weak seals that fail during handling or transit. Overwrappers and cartoners with pneumatic or spring-loaded sealing heads—where pressure is fixed and heat is time-based—can't adapt to cellulose materials as effectively as servo-driven systems that adjust both parameters dynamically. The outcome is either higher reject rates or line speed reductions to allow longer dwell times.
Dimensional variation in moulded cellulose trays and recycled cartonboard creates handling problems for pick-and-place systems and blank feeders. If tray depth or carton blank dimensions vary by more than a millimetre or two, machinery designed for tight-tolerance plastic trays or virgin board will misalign, jam, or reject parts. Vision systems and servo-driven adjustments can compensate for some variation, but only if the machinery was specified with that capability in the first place.
Static and dust generation increase with cellulose substrates, particularly recycled board. Dust fouls photoelectric sensors, clogs vacuum filters, and contaminates sealing surfaces. Static causes carton blanks to stick together during feeding or attract loose fibres that interfere with printing registration. Machinery without adequate dust extraction, sensor protection, or anti-static measures will see more frequent stoppages and higher maintenance requirements when running cellulose materials.
A real example: a snack manufacturer switched from BOPP film to a cellulose-based alternative for multipack overwraps. Their existing overwrapper, rated at 80 packs per minute on conventional film, averaged 55 on cellulose because the fixed-tension film feed couldn't adapt to the material's lower elongation. Reject rates increased from 2% to 7% due to torn film and weak seals. The substrate switch met the sustainability target but cost them 30% throughput until they upgraded to an overwrapper with servo-controlled film handling.
How Machinery Specification Solves Cellulose Substrate Challenges
Servo-driven film tension control is essential for cellulose-based overwrapping. Systems that adjust tension dynamically based on material feedback, using load cells or torque monitoring, maintain consistent film handling across different cellulose grades without manual recalibration. This is important because cellulose film properties vary between suppliers and even between production lots, and machinery that requires operator intervention for every material change will lose efficiency quickly.
Adjustable sealing parameters allow reliable performance across cellulose substrates. Sealing heads with independent control over temperature, pressure, and dwell time can adapt to different cellulose films and coatings without compromising seal integrity or material quality. Servo-driven sealing systems also enable faster changeovers between materials, because parameters are stored digitally per recipe rather than requiring mechanical adjustment.
Vacuum systems designed for dust-prone substrates include inline filtration, self-cleaning valves, and positive pressure purging to prevent clogging. Blank feeders and tray handlers that will run recycled cellulose board should have protected sensors, easy-access filter changes, and air knives to clear loose fibres before they reach critical handling points. These features are baseline requirements if cellulose substrates are part of your material roadmap.
Forming and compression systems with variable pressure prevent damage to lightweight cellulose cartons and trays. Fixed-pressure systems designed for heavier board grades will crush or distort cellulose panels during forming, especially on recycled or low-density substrates. Servo-controlled forming rails and adjustable hold-down guides maintain consistent carton geometry without over-compressing the material, which improves both pack quality and line speed.
Integration with material suppliers matters more with cellulose substrates than with conventional materials. Cellulose film and board properties (moisture content, tensile strength, seal initiation temperature) vary more widely than plastic equivalents, and machinery performance depends on staying within the material's processing window. Working with substrate suppliers who can provide consistent specifications and with machinery suppliers who understand how those specs translate to machine settings reduces trial-and-error during material transitions.
What's Driving Cellulose Adoption and What to Plan For
Extended producer responsibility legislation is accelerating cellulose adoption across Europe. Packaging that can't be recycled or composted within existing municipal systems will carry higher fees or outright restrictions, which makes cellulose-based alternatives commercially necessary, not just environmentally preferable. Manufacturers planning capital investments in secondary packaging machinery should assume cellulose substrates will be part of their material mix within two years, even if they're running conventional materials today.
Retailer mandates for plastic reduction are creating specification pressure at brand level. Major UK and European retailers are setting targets for eliminating non-recyclable plastic from own-label products, which means brands supplying those retailers must reformulate packaging or lose shelf space. Secondary packaging machinery that can't handle cellulose films, recycled board, or moulded fibre trays becomes a bottleneck when those reformulations happen, because production schedules don't pause for machinery upgrades.
Material innovation is moving faster than machinery replacement cycles. New cellulose-based films, coatings, and moulded structures are being commercialised continuously, and their processing requirements vary. Machinery specified today needs to be adaptable enough to handle materials that don't yet exist in volume production, which means prioritising flexibility (adjustable parameters, digital recipe storage, modular tooling) over fixed-specification systems optimised for a narrow material range.
Cost parity between cellulose and conventional substrates is improving but not yet universal. Cellulose films remain more expensive than polyethylene equivalents in most categories, though the gap is narrowing as production scales. For manufacturers, this means the economic case for cellulose adoption depends heavily on minimising performance loss during the transition. Machinery that maintains line speed and reject rates on cellulose substrates makes the material cost difference easier to absorb than machinery that forces throughput reductions or quality compromises.
Service and technical support become more critical when running new substrates. Cellulose materials introduce variables that even experienced operators and maintenance teams may not have encountered, different failure modes, unfamiliar troubleshooting steps, material-specific adjustments. Machinery suppliers with application engineering support, substrate testing capabilities, and responsive technical service help manufacturers navigate material transitions without extended trial periods or production losses.
If you're evaluating cellulose-based substrates to meet sustainability targets or retailer requirements, machinery capability needs to be part of the decision from the start. Running cellulose films, recycled board, or moulded trays on secondary packaging lines designed for conventional materials will cost you throughput, quality, or both. Jacob White supplies and supports secondary packaging machinery built to handle substrate variability, contact us to discuss what your material roadmap requires.