

Multipack Carton Packaging for Snack Bars, Cereals and Wrapped Products
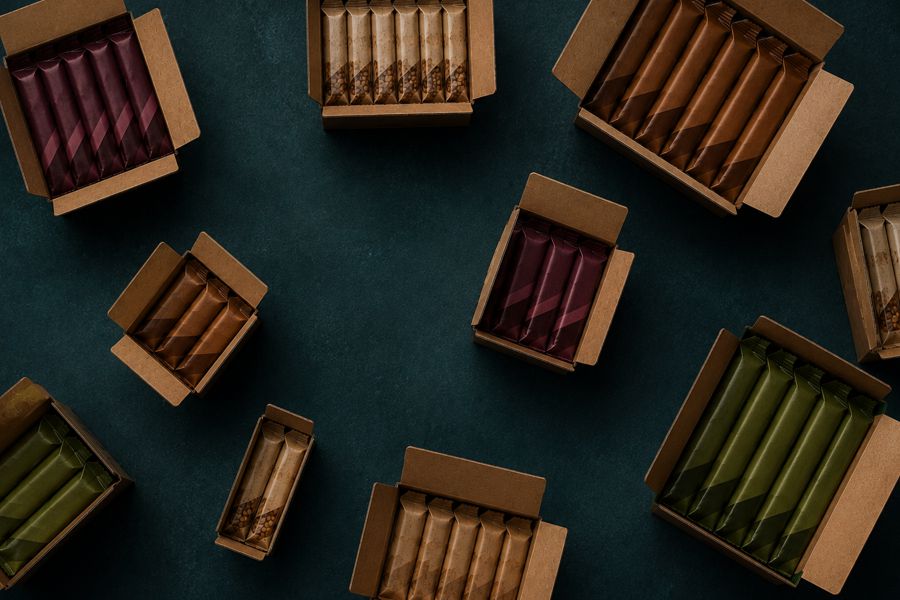
A multipack carton is a retail packaging format that groups a fixed count of individually wrapped products into a single carton for sale as one unit. The carton might hold four protein bars, eight cereal bars, six breakfast biscuit packs, or twelve individual snack portions, the count and format vary by product category and retail channel, but the fundamental challenge is consistent, which is individual primary packs need to be counted accurately, collated into the correct orientation and group size, and loaded into a carton reliably at production speed.
That process sounds straightforward, but in practice, the secondary packaging line running multipack cartons is where a significant proportion of production efficiency is determined, and where under-specified machinery shows up quickly in output figures, waste rates and changeover costs.
Where multipack cartons sit in the packaging structure
It helps to be clear about what multipack cartons are and are not. They are a secondary packaging format, they group primary packs, not primary product. The primary pack is the individual flowrap, pillow pack or sealed film that contains the product itself. The multipack carton sits around a defined count of those primary packs and presents them to retail as a single purchase unit.
This distinguishes the multipack carton from a shipper or transit case, which groups multiple retail units for distribution rather than for shelf presentation, and from a shelf-ready carton, which is designed to be opened and placed directly on shelf as a display unit. Multipack cartons are sold to the end consumer intact, the carton itself is part of the retail proposition, carrying branding, nutritional information and count claims.
For snack bars, cereals and similar wrapped products, multipack cartons are the dominant retail format in grocery multiples. The count per carton is often dictated by the retailer rather than the manufacturer, a specific facing requirement, a price-point calculation, or a promotional variant running alongside the standard count. That retailer-driven count flexibility is one of the reasons multipack lines need to handle format changes efficiently.
How a multipack carton line runs
The sequence on a multipack cartoning line follows a consistent pattern regardless of the specific product.
Infeed and singulation
Primary packs arrive from the upstream primary packaging equipment, a flowrapper, form-fill-seal machine or similar, in a continuous or batched stream. At this point they need to be singulated: separated into a controlled, evenly spaced single file so the collation system can count and group them accurately. Infeed conveyor design, lane width and product spacing all affect how reliably this happens with the primary pack format being run.
Collation
The collation system counts primary packs into the required group size and forms them into the orientation needed for carton loading, lying flat, standing on edge, or in a specific stacked arrangement. For multipack cartons, collation is particularly critical because the retail count claim on the pack must be exact. A collation error that puts seven bars into an eight-count carton is not merely a machine efficiency problem, it is a compliance and customer issue.
Collation systems vary in how they handle count changes. Some require mechanical adjustment when the group size changes; others use configurable lane and gate settings that can be adjusted more quickly. On a line running promotional variants alongside standard counts, the collation system's ability to change group size without extended downtime is a meaningful specification consideration.
Carton erection and loading
Flat-pack carton blanks are erected by the cartoner, formed from flat board into an open carton, and the collated group is then loaded. For most snack bar and cereal multipack formats, horizontal end-loading is the standard approach: the collated group is pushed horizontally into the open carton end, which is then closed and sealed. Top-loading formats are used where product geometry or fragility makes end-loading unsuitable.
Closing and coding
Once loaded, the carton is closed, by tuck, glue or a combination, coded with batch and date information, and discharged for downstream handling. The coding stage needs to apply a clear, durable mark on a surface that the carton board and print finish will accept reliably.
Downstream
Finished multipack cartons typically move to a case packer or manual pack-off point, and then to palletising. For high-volume lines, the downstream equipment needs to match the cartoner's output rate; bottlenecks at case-packing or palletising cancel out cartoner efficiency gains.
Where multipack lines lose performance
The gap between rated machine capacity and actual average output is a persistent issue on multipack cartoning lines, and the causes are usually the same across different products and formats.
Changeover time
A multipack line running a single SKU in a stable count and carton size is relatively simple to optimise. Most multipack lines do not run a single SKU. Promotional counts, seasonal variants, retailer-specific packs and product range extensions mean that format changes, different group size, different carton dimensions, or both, are a regular occurrence. On manually adjusted machinery, a full format change can absorb sixty to ninety minutes of productive time. On a line with two or three format changes per day across multiple SKUs, that adds up to a significant proportion of available capacity.
Tool-less or quick-release format change systems reduce this substantially. When the components that control lane width, carton size and collation group size can be adjusted to pre-set positions without tools, changeover times that previously took an hour can be reduced to fifteen or twenty minutes. The machine does not need to run faster, it runs more of the shift.
Collation accuracy under variation
Primary packs are not perfectly uniform. Film tension varies, seal profiles differ slightly between runs, and product density affects how firmly the pack holds its shape. A collation system with tight tolerances and no adjustment latitude will generate jams and rejects when primary pack variation is at the higher end of normal. Designing reasonable tolerance into the infeed and collation system, and fitting upstream rejection for clearly malformed packs before they reach collation, reduces the interruption rate on the cartoning line.
Carton board handling
Not all cartonboard runs the same way. Lighter board grades, high-coverage print finishes, and recycled-content board all behave differently in the erection and closing stages compared with heavier virgin board. A machine calibrated for one board specification that is then asked to run a lighter or more recycled grade may see erection failures, flap-closing problems or glue adhesion issues that reduce yield. Specifying a machine with a broad substrate operating range, and a glue system with sufficient temperature and viscosity flexibility, reduces the risk when board specifications change, as they are increasingly likely to do given retailer and regulatory pressure on packaging sustainability.
Glue system performance after stops
Planned and unplanned line stops both create a settling period when the line restarts. Glue systems that recover quickly to operating temperature and viscosity after a stop reduce the waste generated at restart and the time before yield returns to acceptable levels. On high-speed multipack lines where even short stops generate a pocket of product that needs to be reworked or discarded, glue system recovery time is a more significant efficiency factor than it might appear on a specification sheet.
Format flexibility and what it demands from the machinery
The commercial pressure on multipack lines is consistently toward more formats, not fewer. Retailers want count flexibility. Promotional calendars require short-run variants. Export markets often demand different count configurations from domestic markets. New product launches add SKUs that need to run on existing equipment.
That pressure makes format flexibility a core specification requirement for multipack cartoning machinery rather than an optional feature. A machine that can handle a six-count and a twelve-count carton in the same bar format without a full mechanical reconfiguration, changing only format parts using tool-less adjustments, is operationally a different proposition from a machine that requires significant downtime between every count change.
For products like cereal bars and snack bars, where the primary pack dimensions are often consistent across SKUs even when the retail count varies, the changeover between multipack sizes is principally a collation group size and carton dimension change rather than a wholesale format change. That makes tool-less changeover especially valuable: the machine does not need to handle radically different product geometries, just different counts and carton sizes, and with the right format-part design that can be done quickly and repeatably.
What buyers should be thinking about when specifying multipack capability
The most useful question when specifying a multipack cartoning line is not what throughput rate is needed, but what the realistic SKU mix and changeover frequency looks like across a twelve-month horizon. A line that needs to run eight different multipack configurations across three product formats, with changeovers happening multiple times per week, has very different specification priorities from a line running two variants at high volume.
The second question is what the primary pack variation looks like. If primary packaging runs tightly and consistently, collation tolerances can be set accordingly. If there is meaningful variation in pack dimensions or firmness across different product runs, the secondary machinery needs enough adjustment range to cope without generating a disproportionate rate of jams and rejects.
Sustainability trajectory matters too. Board specifications are changing, and a line specified today may need to run lighter or more recycled-content board within its operational life. Selecting machinery with broad substrate tolerance from the outset is cheaper than retrofitting adjustments later.
Jacob White works with manufacturers across snack, cereal and confectionery categories to specify secondary packaging lines that handle real-world SKU complexity, contact us to discuss what your multipack line actually needs.