

Tissue Embossing Determines Pack Stability and Line Performance
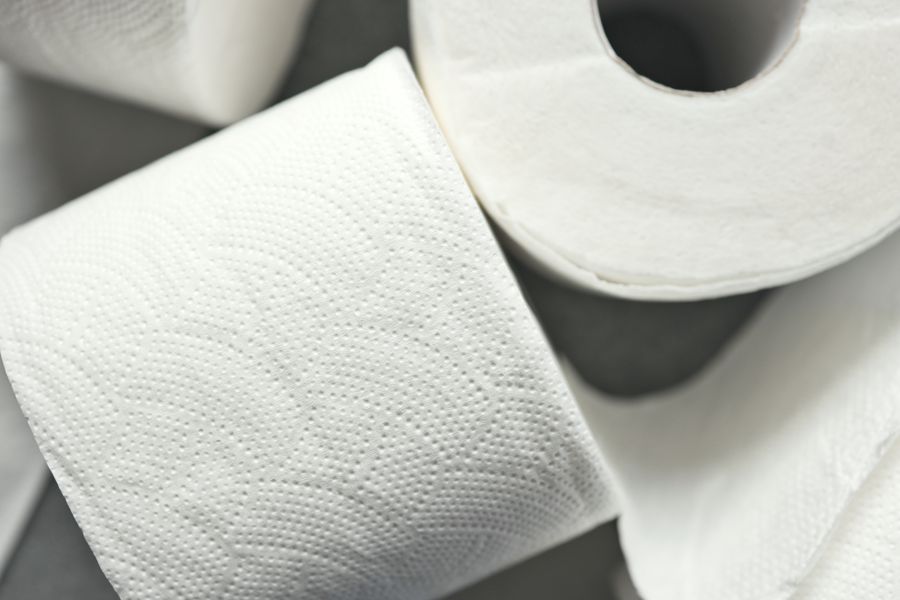
Tissue embossing is the process of creating raised patterns on tissue paper using engraved steel rollers under controlled pressure and temperature. It adds texture, improves absorbency, increases bulk without adding weight, and creates visual differentiation between products. Embossing happens during tissue converting, after the parent reel is unwound and before it's cut, folded, or wound into finished rolls. For manufacturers running secondary packaging lines that handle embossed tissue products, the embossing pattern and depth directly affect how reliably cartoners, overwrappers, and multipack bundlers can handle the finished product.
Embossed tissue rolls have different compression characteristics than un-embossed equivalents. The raised pattern creates air pockets within the roll structure, which means diameter varies more under handling pressure, pack firmness changes depending on how tightly the tissue was wound, and stack stability in multipack formats depends on whether the embossing pattern nests or creates gaps between rolls. If your secondary packaging machinery was specified around un-embossed tissue or a single embossing style, switching patterns or depths without adjusting machine settings will result in misaligned packs, inconsistent compression during overwrapping, or unstable stacks that fail quality checks.
The commercial pressure to differentiate tissue products through embossing; deeper patterns, multi-ply embossing, branded textures; creates variability that secondary packaging machinery must handle without performance loss. Machinery that can't adapt to embossing differences becomes a constraint when product development introduces new patterns or when retail customers specify custom embossing for own-label ranges.
How Tissue Embossing Affects Secondary Packaging Operations
Tissue embossing influences pack dimensions, handling characteristics, and stack behaviour in ways that matter at secondary packaging level. Embossed toilet rolls and kitchen towels enter secondary packaging lines as individual finished rolls, multipacks, or pre-grouped bundles. The machinery handling this work; horizontal cartoners, shrink bundlers, tray formers, flow wrappers; must account for embossing-related variation in roll diameter, compression resistance, and surface friction.
Embossed rolls compress more than un-embossed rolls under the same pressure, but the degree of compression varies with embossing depth and pattern density. A deeply embossed decorative pattern compresses more than a shallow micro-embossing, which means pack dimensions can vary even when the base tissue specification remains constant. Cartoners with fixed lane width or height settings will struggle to handle embossing variation without rejecting packs or creating loose cartons that shift during transit.
Surface friction changes with embossing pattern. Raised textures increase contact area and can create higher static friction between rolls during handling, which affects infeed timing, lane separation, and whether rolls move cleanly through forming and loading stations. Overwrappers and flow wrappers that rely on predictable product sliding behaviour will see timing issues when embossing patterns change, particularly if the machinery uses mechanical cam systems rather than servo-driven motion control.
Stack stability in multipack formats depends on how embossing patterns interact between layers. Some embossing designs nest; the raised pattern on one roll fits into the recessed areas of the adjacent roll; which improves stack firmness. Other patterns create gaps, which makes stacks less stable and more prone to shifting inside cartons or shrink bundles. Secondary packaging machinery that applies fixed compression during bundling or case packing may over-compress nested patterns or fail to stabilise non-nesting designs, depending on how it was set up.
What Breaks When Embossing Variability Isn't Managed
The most common failure mode is dimensional inconsistency during cartoning. If embossed roll diameter varies by more than a few millimetres between production batches; because embossing depth changed, winding tension wasn't consistent, or a different parent reel was used; cartoners with fixed-height or fixed-width settings will either jam, create loose packs, or reject product. The machinery isn't faulty; it's responding to variation the specification didn't account for.
Compression damage occurs when secondary packaging machinery applies too much pressure to deeply embossed tissue. Shrink bundlers, overwrappers, and case packers that use pneumatic or spring-loaded compression to stabilise packs can crush embossing patterns if the pressure wasn't calibrated for the material. Crushed embossing reduces perceived product quality, affects absorbency claims, and creates customer complaints; even though the tissue itself is undamaged.
Timing and registration issues appear when surface friction changes between embossing styles. Infeed conveyors, lane dividers, and product handling systems calibrated for one embossing pattern may mistime or misalign when a new pattern is introduced, particularly if the change happens mid-shift without machine recalibration. The result is product jams, partial carton loads, or downstream stoppages that operators attribute to "the line running badly" rather than embossing-related friction differences.
Stack instability in multipacks shows up as cartons that shift during handling or transit. If embossing patterns don't nest, or if the machinery isn't applying enough compression to stabilise non-nesting designs, finished multipacks will have internal movement that causes carton distortion, torn overwrap, or retail rejection. The issue isn't the packaging format; it's the mismatch between embossing behaviour and how the machinery was set to handle it.
A real example: a tissue converter introduced a new premium embossing pattern with 40% deeper texture than their standard product. Their existing horizontal cartoner, set up for the original embossing depth, began rejecting 12% of packs because roll diameter variation exceeded the machine's tolerance. Adjusting lane guides and compression settings reduced rejects to 3%, but only after two days of trial runs and lost production time. The embossing change was commercially necessary; the machinery just wasn't ready for it.
How Machinery and Specification Choices Solve Embossing Challenges
Servo-driven lane adjustment allows cartoners and case packers to handle embossing-related dimensional variation without manual recalibration. Systems with motorised width and height guides can switch between product formats; or accommodate batch-to-batch variation; using stored digital recipes rather than spanners and shims. This matters when running multiple embossing patterns across a production week, or when embossing depth varies slightly between parent reels.
Adjustable compression control prevents damage to deeply embossed tissue during bundling and overwrapping. Servo-controlled compression heads that modulate pressure based on product feedback; using load cells or torque monitoring; can apply enough force to stabilise packs without crushing embossing patterns. Pneumatic systems with pressure regulators offer some flexibility, but they don't adapt dynamically to product variation the way servo systems do.
Vision systems and sensor technology improve handling consistency when embossing affects surface appearance or friction. Cameras that detect roll position and orientation before loading, or sensors that measure pack height dynamically during cartoning, allow machinery to adjust handling parameters per pack rather than assuming uniform dimensions. This reduces rejects when embossing creates dimensional variation that fixed mechanical systems can't accommodate.
Infeed timing control compensates for embossing-related friction changes. Servo-driven conveyors and lane dividers maintain consistent product spacing and alignment even when surface friction varies between embossing patterns. Mechanical systems that rely on fixed belt speeds or cam-driven pushers will lose timing precision when embossing changes, which creates downstream handling issues that are difficult to troubleshoot without understanding the root cause.
Integration between converting and secondary packaging operations reduces embossing-related variability before it reaches the cartoner or overwrapper. If tissue winding tension, embossing pressure, and roll diameter are monitored and controlled during converting, the dimensional variation that secondary packaging machinery must handle is minimised. This requires communication between converting and packaging teams, and ideally shared data systems that flag when embossing parameters drift outside tolerance.
Embossing Trends and What Buyers Should Plan For
Premium embossing is increasing as tissue manufacturers differentiate through texture and visual appeal. Deeper patterns, multi-layer embossing, and branded designs are all becoming more common, particularly in retail own-label and premium segments. Secondary packaging machinery specified today should assume embossing depth and pattern density will increase, which means prioritising adjustability and compression control over fixed-specification systems.
Sustainable tissue substrates are changing embossing behaviour. Recycled tissue, bamboo-based products, and alternative fibres don't emboss identically to virgin pulp. Pattern definition varies, compression characteristics differ, and some alternative fibres are more prone to embossing collapse under handling pressure. Machinery buyers planning to run sustainable tissue products should test embossing compatibility during equipment trials, not assume performance will match conventional materials.
Custom embossing for retail customers creates SKU proliferation at secondary packaging level. Own-label ranges with retailer-specific embossing patterns mean more format changes, tighter production windows, and higher pressure on changeover speed. Secondary packaging machinery that requires extended setup time between embossing variants becomes a bottleneck when customer demands shift toward shorter runs and faster turnaround.
Automation in tissue converting is improving embossing consistency, which benefits secondary packaging performance. Modern embossing rollers with servo-driven pressure control, automated nip adjustment, and real-time monitoring reduce roll-to-roll dimensional variation. As converting technology improves, secondary packaging machinery should be capable of exploiting that consistency; faster line speeds, tighter pack tolerances, reduced reject rates; rather than being limited by legacy handling systems designed for wider variation.
Service and application support become more valuable when running variable embossing patterns. Machinery suppliers who understand tissue embossing behaviour, can recommend compression settings per pattern type, and provide responsive troubleshooting when new embossing designs cause handling issues add operational value that purchase price alone doesn't capture. Tissue manufacturers running multiple embossing styles benefit more from suppliers with application engineering expertise than from the cheapest cartoner on the market.
Moving Forward
If you're running embossed tissue products through secondary packaging lines, or if you're introducing new embossing patterns to differentiate products, the machinery handling those products needs to match embossing variability. Fixed-adjustment systems, rigid compression settings, and mechanical timing controls will struggle with the dimensional and friction differences that embossing creates. Jacob White works with manufacturers to solve secondary packaging challenges, contact us to discuss what your line actually needs.